Wastewater management is an important part of modern industrial and municipal operations. Residential buildings, commercial facilities, manufacturing units, and treatment plants require reliable pumping equipment to manage wastewater and maintain proper drainage systems. Choosing suitable pumps helps move wastewater efficiently and reduces the risk of blockages and operational problems.
Different applications require different pumping technologies depending on the type of liquid, solid content, flow rate, and installation conditions. This is why selecting experienced Sewage Submersible Pump Manufacturers is important for businesses looking for dependable wastewater handling solutions.
Understanding Sewage Submersible Pumps and Their Applications
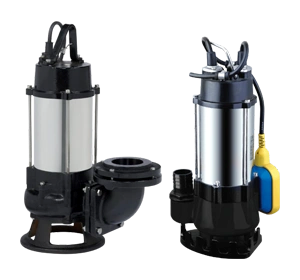
A sewage submersible pump is designed to operate while completely or partially submerged in the liquid being pumped, according to its design. It uses an electric motor and an impeller to move wastewater from one location to another.
These pumps are commonly used in sewage treatment plants, drainage systems, municipal wastewater facilities, commercial buildings, and industrial applications. Depending on their design, they can handle wastewater containing suspended solids and other impurities.
Professional Sewage Submersible Pump Manufacturers focus on developing pumping equipment that supports reliable wastewater transfer under different operating conditions.
Important Features of Sewage Submersible Pumps
Submerged Operation: These pumps are designed to work underwater, making them suitable for sumps, sewage pits, and wastewater collection systems.
Solids Handling: Suitable models can handle wastewater containing suspended solids, depending on impeller design and passage size.
Space-Saving Installation: Their submerged arrangement can reduce the need for separate surface pumping installations.
Multiple Applications: These pumps are used in sewage treatment, drainage, construction, and industrial wastewater management.
Before purchasing, businesses should evaluate flow rate, discharge head, solid-handling capacity, motor protection, and liquid characteristics. Reliable Sewage Submersible Pump Manufacturers can help buyers identify suitable equipment for their specific requirements.
Why Choose Filter Press Pump Manufacturers for Industrial Filtration?
Many industries use filtration systems to separate solid particles from liquids during their production processes. Filter press systems are commonly used in chemical processing, mining, pharmaceuticals, wastewater treatment, and manufacturing.
A filter press pump supplies liquid under the required pressure to a filter press, where suspended solids are separated from the liquid through filter plates and filter media.
Experienced Filter Press Pump Manufacturers develop pumping solutions according to filtration requirements, slurry characteristics, operating pressure, and flow conditions.
Key Benefits of Filter Press Pumps
Efficient Slurry Transfer: These pumps are designed to transfer slurry into filter press systems.
Pressure-Based Operation: Suitable pump designs help provide the pressure required during different stages of filtration.
Industrial Applications: They are used in chemical plants, mining operations, wastewater treatment facilities, and other filtration processes.
Application-Specific Design: Pump selection depends on slurry concentration, particle size, required pressure, and filtration capacity.
Before choosing a filter press pump, buyers should check slurry properties, operating pressure, flow rate, material compatibility, and maintenance requirements. Professional Filter Press Pump Manufacturers can help businesses select suitable equipment for their filtration operations.
Understanding Polypropylene Pump Manufacturers and Their Industrial Applications
Industrial facilities often handle chemicals and corrosive liquids that require specialised pumping equipment. Using unsuitable pump materials can result in corrosion, leakage, and unnecessary maintenance costs.
Polypropylene pumps are manufactured using a thermoplastic material known for its lightweight construction and resistance to many chemicals. These pumps are commonly used in chemical processing, electroplating, wastewater treatment, and industrial liquid transfer.
Reliable Polypropylene Pump Manufacturers focus on producing pumps that meet different fluid-handling requirements while considering chemical compatibility and operating conditions.
Important Features of Polypropylene Pumps
Lightweight Construction: Polypropylene is lighter than many traditional metal materials, which can make handling and installation easier.
Chemical Resistance: It offers resistance to many acids and alkalis, depending on chemical concentration and temperature.
Corrosion Protection: Suitable polypropylene construction can help reduce corrosion-related issues in compatible applications.
Wide Industrial Applications: These pumps are used in chemical processing, electroplating, water treatment, and industrial manufacturing.
Before selecting a polypropylene pump, businesses should evaluate the chemical properties of the liquid, temperature limits, pressure requirements, and flow capacity. Experienced Polypropylene Pump Manufacturers can provide guidance on suitable materials and pump configurations.
How to Choose the Right Industrial Pump Manufacturer
Selecting a reliable manufacturer is important for maintaining smooth industrial operations. Businesses should compare product quality, technical specifications, and manufacturing experience before purchasing pumping equipment.
Here are some important factors to consider:
Manufacturing Quality: Check the construction materials, pump design, and manufacturing standards.
Technical Specifications: Evaluate flow rate, pressure, temperature limits, and solid-handling capacity.
Material Compatibility: Ensure the pump materials are suitable for the liquid or slurry being transferred.
Product Range: Explore different pumping solutions to find equipment suitable for your application.
Customer Support: Consider technical guidance, maintenance assistance, and product information.
Comparing these factors helps businesses make informed decisions and select equipment that meets their operational requirements.
Why Choose JEE Pumps Limited?
When looking for dependable industrial pumping equipment, businesses should consider manufacturers that understand different fluid-handling requirements. JEE Pumps Limited offers industrial pumping solutions for various applications across different industries.
Choosing suitable pumping equipment requires understanding liquid properties, flow rate, operating pressure, solid content, and installation conditions. These factors help determine the right pump design for each application.
Whether a business requires equipment for wastewater management, industrial filtration, or chemical transfer, selecting the correct pump material and configuration is important for reliable performance.
JEE Pumps Limited is a manufacturer businesses can explore when looking for industrial pumping solutions. Buyers should review product specifications and discuss their application requirements to identify suitable equipment.
Conclusion
Choosing the right industrial pump is essential for maintaining efficient fluid handling and smooth operations. Sewage submersible pumps support wastewater management, filter press pumps help with industrial solid-liquid separation, and polypropylene pumps provide solutions for transferring many compatible chemicals. Businesses should compare material quality, technical specifications, operating conditions, and maintenance requirements before making a purchase. JEE Pumps Limited is a manufacturer businesses can explore for dependable industrial pumping solutions.